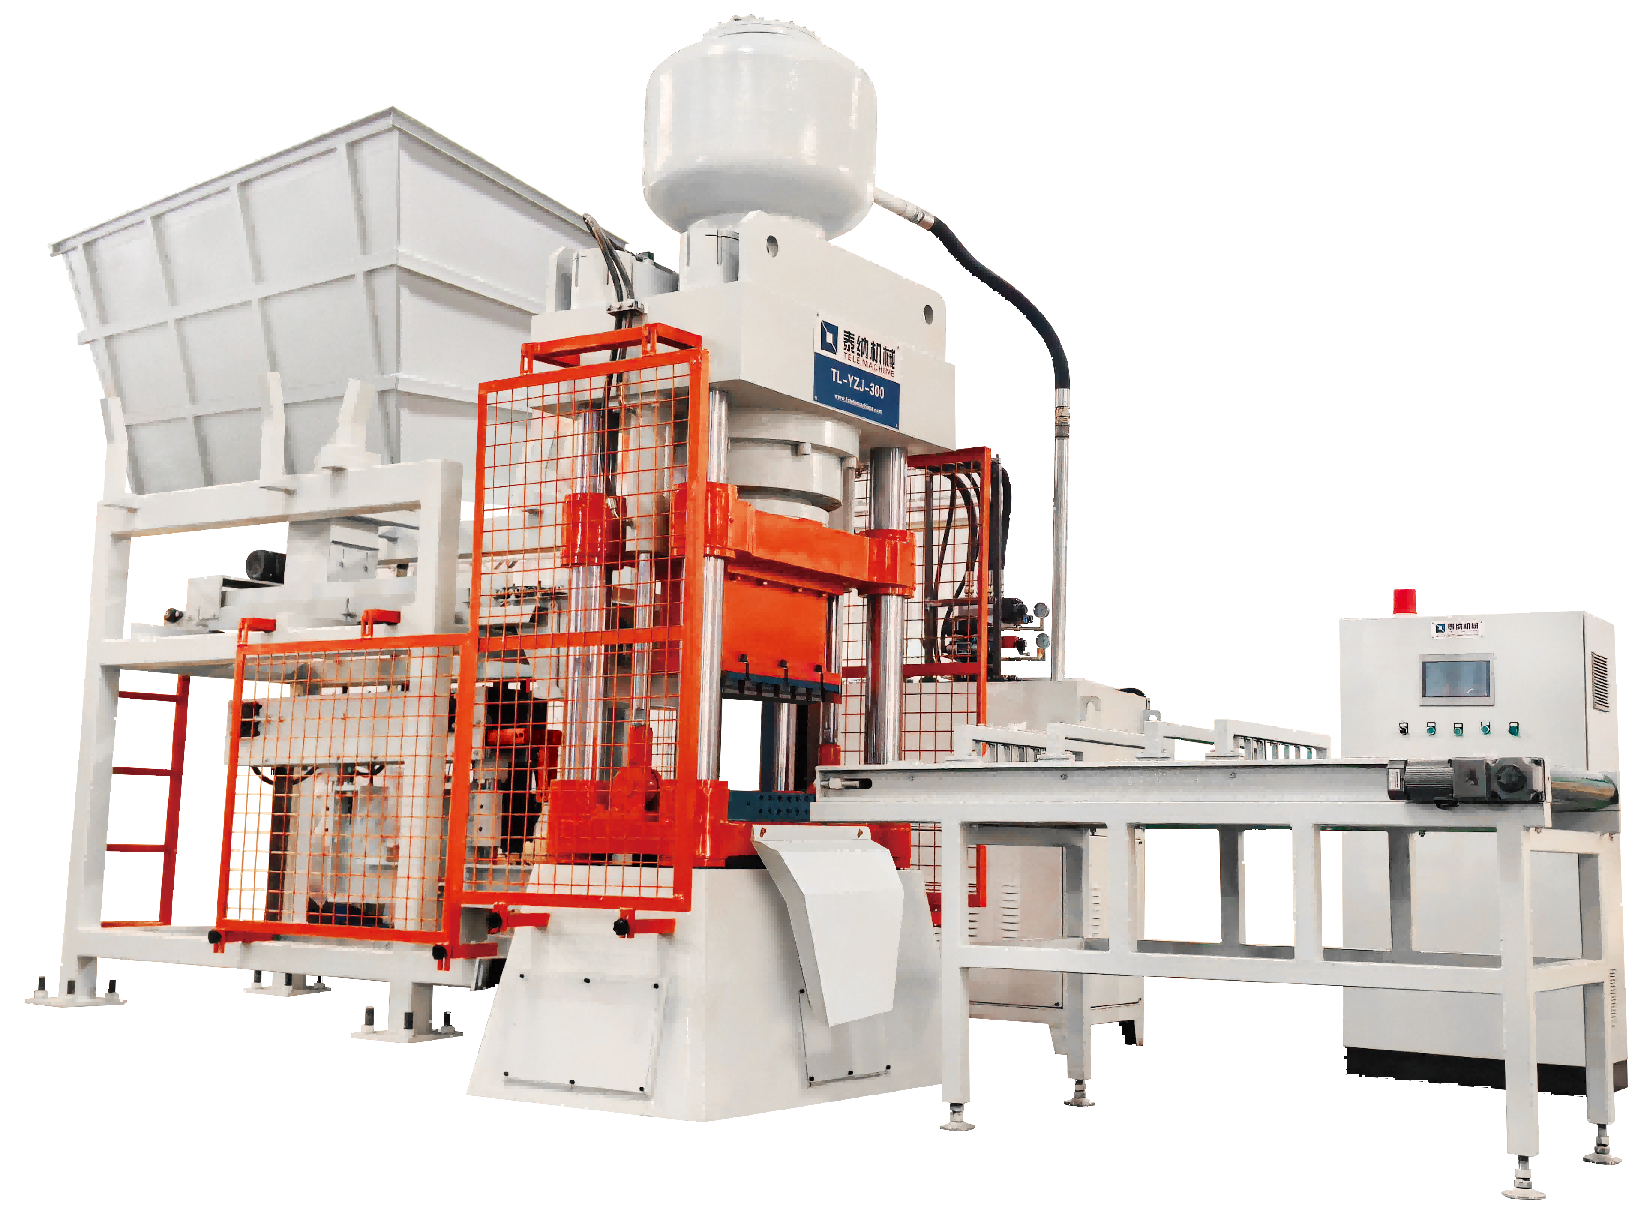
C21-11. Auto Hydraulic Tiles & Bricks Press Type TL-YZJ-300
C21-11. Auto Hydraulic Tiles & Bricks Press Type TL-YZJ-300
C21-11. Auto Hydraulic Tiles & Bricks Press Type TL-YZJ-300
| Parameter | YZJ-300 |
|---|---|
| Dimension L×W×H (mm) | 3332×3257×1385 |
| Working Table L×W (mm) | 820×500 |
| Working Frequency (1/min) | 4~6 |
| Lower Ejecting Force (kN) | 300 |
| Lower Ejecting Stroke (mm) | 120 |
| Max Press Force (kN) | 3000 |
| Motor Power (kw) | 41.5 |
| Weight (kg) | 8800 |
Machine Features
- This machine is a fully automatic brick forming equipment, material distribution, pressing and molding, and de-molding operate automatically according to the set program, enabling unattended operation. The pressing pressure, exhaust frequency, exhaust time, brick blank thickness, etc. can all be set on the control panel, featuring high working efficiency and large output. It has the dvantages of making “thick & special shapes bricks”, lies across a full thickness range of 6mm to 80 mm. If the user configures a conveyor line and a palletizer in the subsequent process, fully automatic assembly line production can be achieved.
- The pressing and shaping of the brick mold is achieved using a patented technology that employs a floating mold frame with bidirectional pressure application, resulting in very small variations and gradual changes in the density of the shaped bricks. This effectively prevents the occurrence of layers within the brick mold, ensuring uniformity in the density of the bricks. The machine also features an automatic adjustment function for the thickness of the brick mold. After the initial setting of the brick mold thickness, it continuously monitors the thickness upon each pressing cycle. If the thickness deviates from the set tolerance, the machine automatically adjusts the feeding height to maintain consistency in the brick mold thickness.
- The floating mold frame method was adopted to achieve uniform density of the brick blank. After molding, the density deviation of the brick blank was small and the density change amplitude was smooth. It avoids the situation where the formation of layers is prone to occur in the middle part of the brick blank in the bidirectional pressurization method.